Residue on processing equipment never announces itself. It creeps. A thin film coats the inside of a barrel. Degraded polymer starts collecting around the die lip. Flow channels narrow by fractions of a millimeter at a time. Nobody sounds the alarm until parts start coming out ugly or the line grinds to a halt for an emergency teardown. By then, the lost production time and scrap costs have already piled up.
What Creates the Mess
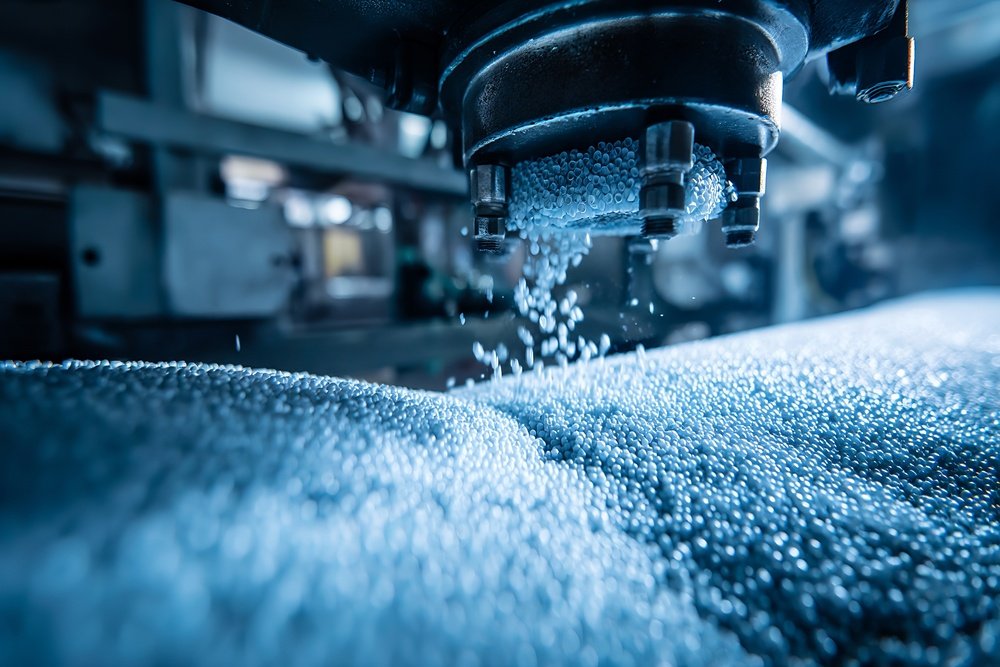
Plastic processing runs hot. Extrusion, injection molding, blown film operations. These machines regularly heat polymers above 400 degrees Fahrenheit. Some go much higher. At those temperatures, polymer chains crack apart. Additives break down or boil off. Lighter molecular fractions in the resin vaporize and settle onto cooler metal surfaces where they bake into a hard, stubborn crust. That crust grabs onto more material with each production cycle. The rougher the surface gets, the faster new residue sticks. It snowballs. Flow paths shrink. Hot spots form where heat can no longer transfer evenly. Finished products pick up streaks, specks, and surface defects that send reject rates climbing.
Keep Temperatures Honest
Cranking up the heat does not automatically improve melt flow. More often it just cooks the resin faster and feeds the buildup problem. Running each barrel zone at the lowest temperature that still delivers good flow is one of the simplest ways to slow residue formation down.
Read More: How Buyback Guarantees Interact With TV on EMI Purchase Agreements
Individual zone monitoring matters more than most operators give it credit for. One thermocouple drifting 15 degrees high can turn a single zone into a degradation factory that contaminates everything downstream. Swapping out tired sensors on a regular schedule keeps displayed temperatures honest. That alone prevents a surprising number of buildup headaches.
Pick Materials That Can Handle the Heat
Resin grade and additive chemistry affect buildup rates more than a lot of processors expect. Some polymer grades carry heavier loads of low molecular weight material that plates out on equipment fast. Others hold together better under thermal stress and leave less behind. Processing aids and internal lubricants make a real difference here too. Synthetic waxes are valued in high-temperature plastic processing for smooth melt flow, reducing die drool, and superior heat resistance. Companies like Trecora provide materials with purity and consistency that ensure cleaner equipment and fewer production stops. A material change like this sometimes outperforms a mechanical solution that costs ten times as much.
Purge Before Things Get Ugly
Waiting for a buildup to force a shutdown is the expensive path. Running a purging compound through the system between jobs or color changes strips degraded material out before it turns to rock. Not all purging compounds are interchangeable though. Temperature range, resin compatibility, and equipment geometry all factor into which one actually works.
Read More: How CFD Traders Access Stock, ETF, and Commodity Opportunities
A compound that cleans a straightforward single-screw extruder might leave dead spots untouched in a complex hot runner system. Getting the match right keeps purge cycles short and effective.
Coat the Metal
Specialty surface coatings on screws, barrels, and die components create a barrier that residue struggles to bond with. Chrome and nickel treatments are common. The slicker the surface stays, the less opportunity degraded polymer has to grab hold and accumulate. Refreshing these coatings during planned maintenance downtime is cheap insurance against the kind of buildup that eventually forces unplanned shutdowns.
Conclusion
Buildup robs throughput quietly and steadily. Tighter temperature control, smarter material choices, regular purging, and maintained equipment surfaces keep it from becoming the silent profit killer it wants to be. The cleanest machine on the floor is almost always the most productive one too.